Insert Molding Services
Overview
Preserved Shop Record: b2b-plastic-injection.com Subject: Insert Molding Services as Practiced in the Preserved Pages The preserved pages of b2b-plastic-injection.com belong to Spro Tech Enterprise Co., Ltd., a mold maker and injection molder whose site language centers on plastic injection molding, double plastic injection mold, die casting mold, and gas assistant plastic mould. The company profile describes an extensive experienced mold maker majoring in plastic injection molding and related mold research for better quality and accommodation of environmental protection. Its high-precision plastic injection mold product and mold making design are described as usable for numerous manufacturing fields, including automobile accessories, household accessories, computer accessories, and many other high-precision products. The product pages list molding for auto part, molding for electronic
Details
and computer, molding for consumer electronic, and molding for motorcycle part. Specific auto-part entries include AB Piller, Back Mirror Consul Set, Big Consul, Computer Cover, Consul Bodies And Part, Consul Covers And Part, automotive parts under consul, cover, electronic back, filler, and filter categories, plus Filter Cover. That is the shop record. The former plant is not quoting from this domain. What follows stays inside that shop's process language and applies it to insert molding services. Insert molding, in the language of this shop, is a plastic injection molding process. It is not a separate department bolted onto mold making. It begins where all of Spro Tech's work begins: at the mold. A mold maker who already builds high-precision plastic injection molds, double plastic injection molds, die casting molds, and gas assistant plastic moulds treats an insert mold as another mold making design problem. The insert is placed into the mold cavity before the plastic is injected. The molten plastic flows around it, encapsulates it, and bonds to it as the part cools. The result is one molded component that carries the insert as a permanent feature rather than as a later assembly step. The preserved product list shows the kind of parts this shop already thinks about. Consul bodies and parts, consul covers and parts, computer covers, back mirror consul sets, big consul, AB piller, electronic back parts, filler parts, and filter covers. Many of those parts are housings, covers, bodies, and structural pieces. Insert molding services fit that same family of work. A consul body can be molded around a metal insert so that a fastener point, a boss, or a mounting feature is formed in place. A computer cover can be molded around a threaded insert so that the cover accepts a screw without a separate pressed-in operation. A filter cover or filler part can be molded around a sleeve, a pin, or a bushing so that the wear surface and the plastic body become one piece. An electronic back part can be molded around a contact or a small metal detail where the plastic must hold it precisely. The shop's process language also includes double plastic injection mold. That matters for insert molding services because a double injection mold can combine materials or colors in one cycle. In insert molding, the same mold discipline applies: the mold is built to hold the insert in a fixed position while the plastic fills the cavity. If the insert shifts, the part shifts. If the mold closes on the insert incorrectly, the insert is damaged or the plastic flashes. So the mold making design must account for insert location, support, and shutoff. The mold maker must decide how the insert is loaded, how it is held during injection, and how the finished part is removed. Those decisions are made at the mold drawing stage, not on the press floor. Gas assistant plastic mould is also part of the preserved language. Gas assist can help where a molded part has thick sections or where pressure must be managed during filling. In insert molding services, gas assist may be considered when the plastic must flow around an insert without over-packing the insert or distorting it. The shop's stated research for better quality and accommodation of environmental protection suggests that process choices are made with quality and material use in mind. Insert molding itself supports that aim because it eliminates secondary assembly steps, reduces separate fasteners, and can reduce the number of loose parts in a final product. The preserved pages describe mold making solutions and universal options for the customer's final satisfaction. In insert molding services, that means the shop does not treat the insert as an afterthought. The insert is part of the mold design. The mold is part of the product design. The product design is part of the manufacturing field, whether that field is automobile accessories, household accessories, computer accessories, or another high-precision product. The same mold maker who builds molds for auto parts, electronic and computer parts, consumer electronic parts, and motorcycle parts can build an insert mold for those same categories. The preserved product names give a practical map. Automotive parts under consul, cover, electronic back, filler, and filter. Filter Cover. Computer Cover. Back Mirror Consul Set. Big Consul. AB Piller. These are not abstract examples. They are the shop's own record of what it molds. Insert molding services extend that record by adding a metal or non-plastic insert into the same kind of molded body, cover, or housing. The insert can be a threaded nut, a stud, a sleeve, a pin, a bushing, a contact, or another preformed piece. The plastic can be a single material or, where a double plastic injection mold is used, more than one material in one cycle. The mold can be a standard high-precision plastic injection mold or a gas assistant plastic mould where the fill pattern calls for it. What the preserved pages do not contain is equally important. There are no prices, no RFQ forms, no street addresses, no phone numbers, no URLs beyond the preserved domain, and no certifications. The record is a shop record: company profile, product categories, mold making, plastic injection molding, double plastic injection mold, die casting mold, gas assistant plastic mould, and the product list. Insert molding services, described in that same language, are a mold making and plastic injection molding service. The insert is placed in the mold. The mold is built to hold it. The plastic is injected around it. The part comes out as one piece. The shop's process language covers the rest: high-precision plastic injection mold product, mold making design, automobile accessories, household accessories, computer accessories, and many other high-precision products. The former plant is not quoting from this domain. This is a preserved shop record, and the topic is insert molding services as that shop would have described them.
Surface finish reference
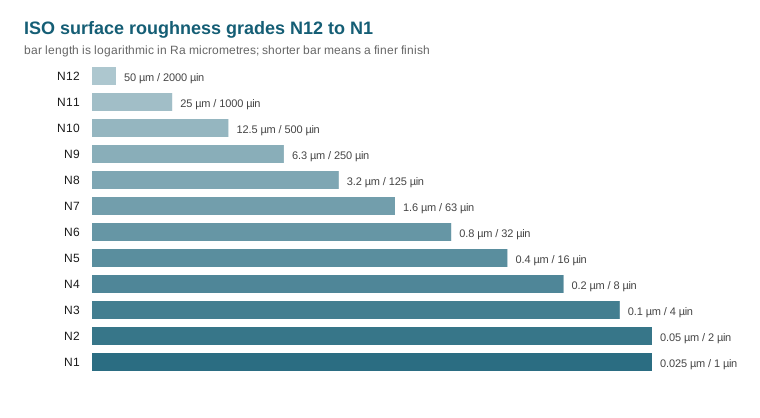
| ISO grade | Ra (µm) | Ra (µin) | RMS (µin) | CLA (µin) | Rt (µm) |
|---|---|---|---|---|---|
| N12 | 50 | 2000 | 2200 | 2000 | 200 |
| N11 | 25 | 1000 | 1100 | 1000 | 100 |
| N10 | 12.5 | 500 | 550 | 500 | 50 |
| N9 | 6.3 | 250 | 275 | 250 | 25 |
| N8 | 3.2 | 125 | 137.5 | 125 | 13 |
| N7 | 1.6 | 63 | 69.3 | 63 | 8 |
| N6 | 0.8 | 32 | 35.2 | 32 | 4 |
| N5 | 0.4 | 16 | 17.6 | 16 | 2 |
| N4 | 0.2 | 8 | 8.8 | 8 | 1.2 |
| N3 | 0.1 | 4 | 4.4 | 4 | 0.8 |
| N2 | 0.05 | 2 | 2.2 | 2 | 0.5 |
| N1 | 0.025 | 1 | 1.1 | 1 | 0.3 |
Common questions
What does N8 surface finish mean?
N8 is Ra 3.2 micrometres, or 125 microinches. The equivalent RMS reading is 137.5 microinch and the CLA figure is 125 microinch. Grades run from N12 (roughest, Ra 50) down to N1 (finest, Ra 0.025).
What does N7 surface finish mean?
N7 is Ra 1.6 micrometres, or 63 microinches. The equivalent RMS reading is 69.3 microinch and the CLA figure is 63 microinch. Grades run from N12 (roughest, Ra 50) down to N1 (finest, Ra 0.025).
What does N5 surface finish mean?
N5 is Ra 0.4 micrometres, or 16 microinches. The equivalent RMS reading is 17.6 microinch and the CLA figure is 16 microinch. Grades run from N12 (roughest, Ra 50) down to N1 (finest, Ra 0.025).
This page is an archival note for informational purposes only. It does not offer representation, evaluate claims, or create a professional relationship.